
Top Chocolate Processing Plant Manufacturers Worldwide?
Choosing among the top Chocolate Processing Plant manufacturers worldwide requires more than comparing equipment prices. It demands evidence about processing performance, food safety, energy use, and long-term technical support. The International Cocoa Organization’s 2023/24 reports highlighted tight cocoa supply and continued volatility in production and grinding markets. These pressures make efficient processing increasingly important. A modern line must protect flavor while reducing waste.
Reliable manufacturers usually provide integrated systems for roasting, refining, conching, tempering, molding, and packaging. Bühler’s chocolate technology publications emphasize process control, recipe consistency, and energy-efficient equipment. Meanwhile, the International Organization for Standardization’s ISO 22000 framework remains a useful reference for food-safety management. These standards do not automatically prove machine quality. Factory execution still matters.
Details reveal the difference. Consider a stainless-steel tempering unit holding stable temperatures, clean transfer pipes, and accessible inspection points. Small design choices can affect cleaning time, product loss, and production continuity. Reports from Grand View Research and Mordor Intelligence also show continued growth in global chocolate demand, although market estimates differ by methodology. That disagreement deserves attention. There is no universally best manufacturer. A supplier may excel in high-volume confectionery production but perform poorly for flexible, small-batch recipes. This guide will compare leading companies through engineering experience, certifications, customization, after-sales service, and documented operating results. Buyers should verify every claim with site visits, reference customers, factory acceptance tests, and total-cost calculations. Machinery is only part of the answer. People, maintenance, and process discipline decide whether a Chocolate Processing Plant performs reliably.
Chocolate Processing Plant Manufacturers: Industry Scope and Core Functions
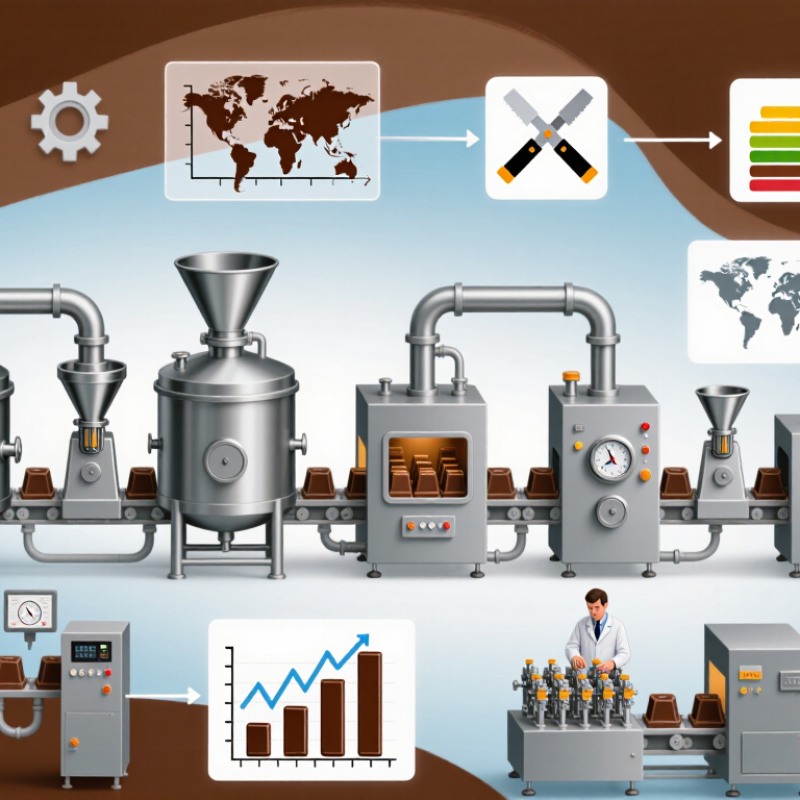
Chocolate processing plant manufacturers serve a demanding part of the food industry. They design and supply equipment for cocoa bean cleaning, roasting, grinding, refining, conching, tempering, molding, and packaging. Their work connects raw materials with stable, market-ready chocolate products.
A capable manufacturer studies the product before recommending machinery. Dark chocolate, milk chocolate, fillings, and compound coatings require different temperature controls and processing times. Hygienic construction is essential. Stainless steel surfaces, accessible inspection points, and controlled drainage help reduce contamination risks. Modern systems may include automated dosing, recipe management, heat recovery, and real-time viscosity monitoring. These features can improve consistency, but they also require trained operators and dependable maintenance.
Quality assurance cannot depend on equipment alone. Manufacturers should provide factory testing, installation guidance, validation records, and clear operating procedures. They also need to understand local food safety expectations, energy limits, production volume, and future expansion plans. Poorly matched machinery can create waste, uneven texture, or costly downtime. That mistake is easy to underestimate.
Practical experience matters. A site visit can reveal problems that drawings miss, such as limited ceiling height or difficult cleaning access. Manufacturers often support spare-parts planning, operator training, and remote troubleshooting after installation. Yet service promises need measurable response times. Technology changes quickly, while basic maintenance discipline still decides many production outcomes.
Top Chocolate Processing Plant Manufacturers Worldwide? - Chocolate Processing Plant Manufacturers: Industry Scope and Core Functions
Industry scope, production stages, equipment functions, quality controls, and application coverage
| Industry Area | Main Processing Stage | Core Equipment or System | Primary Function | Typical Control Point | Common Applications |
|---|---|---|---|---|---|
| Cocoa Bean Preparation | Cleaning and foreign-material removal | Cleaning units, sieves, magnets, aspiration systems | Removes stones, dust, metal particles, and other contaminants before roasting | Foreign-material detection and bean-size separation | Cocoa liquor, cocoa butter, and cocoa powder production |
| Roasting | Thermal treatment of cocoa beans or nibs | Batch or continuous roasters | Develops cocoa flavor, reduces moisture, and improves microbial control | Time, temperature, moisture, and airflow | Dark, milk, and white chocolate ingredients |
| Winnowing | Removal of cocoa shell | Crackers, nib separators, and air-classification systems | Separates cocoa nibs from shells after roasting | Shell content and nib recovery rate | Cocoa liquor and nib-based products |
| Grinding and Liquor Production | Size reduction of cocoa nibs | Nibs grinders, pre-grinders, and refining mills | Converts nibs into a fluid cocoa mass known as cocoa liquor | Particle size, temperature, viscosity, and fat release | Chocolate recipes, cocoa butter extraction, and cocoa powder processing |
| Pressing and Powder Processing | Separation of cocoa butter and cocoa solids | Hydraulic cocoa presses, cake breakers, and powder mills | Produces cocoa butter and cocoa powder with controlled fat content | Residual fat percentage, powder fineness, and bulk density | Bakery, beverage, confectionery, and dairy applications |
| Ingredient Mixing | Blending of cocoa, sugar, milk solids, and fats | Batch mixers, continuous mixers, and dosing systems | Creates a uniform chocolate mass according to the product formulation | Recipe accuracy, mixing time, and mass temperature | Bars, pralines, coatings, fillings, and compound products |
| Refining | Particle-size reduction | Five-roll refiners and alternative refining mills | Reduces sugar and cocoa particles to create a smoother mouthfeel | Particle-size distribution and product consistency | Premium chocolate, filled products, and couverture-style products |
| Conching | Flavor development and moisture reduction | Longitudinal or rotary conches | Improves flavor, viscosity, texture, and aroma through controlled agitation and aeration | Time, temperature, airflow, moisture, and viscosity | Dark, milk, and white chocolate production |
| Tempering | Controlled crystallization of cocoa butter | Continuous or batch tempering machines | Forms stable cocoa-butter crystals for gloss, snap, and demolding performance | Temperature profile and crystal formation | Molded bars, pralines, enrobed centers, and decorations |
| Molding and Depositing | Forming liquid chocolate into defined shapes | Chocolate depositors, molds, vibrating tables, and cooling tunnels | Produces consistent solid or filled chocolate pieces | Deposit weight, mold temperature, cooling profile, and demolding quality | Bars, tablets, pralines, seasonal shapes, and inclusions |
| Enrobing | Coating centers with chocolate | Enrobing lines, wire belts, chocolate curtains, and cooling tunnels | Applies a controlled chocolate layer around biscuits, wafers, bars, or fillings | Coating weight, belt speed, viscosity, and cooling temperature | Biscuits, wafers, snack bars, fruits, nuts, and confectionery centers |
| Filling and One-Shot Production | Simultaneous depositing of shell and filling | One-shot depositors, filling tanks, and temperature-controlled pipelines | Creates filled chocolates with controlled shell thickness and filling volume | Filling ratio, viscosity, temperature, and allergen separation | Cream centers, ganache-style fillings, caramel, and nut-based fillings |
| Cooling and Setting | Controlled solidification | Cooling tunnels, refrigerated rooms, and humidity-control systems | Sets chocolate without excessive condensation, bloom, or deformation | Air temperature, relative humidity, residence time, and product-core temperature | Molded, enrobed, and filled chocolate products |
| Packaging and End-of-Line Handling | Wrapping, cartoning, inspection, and case packing | Flow wrappers, foil wrappers, cartoners, checkweighers, and metal detectors | Protects products from oxygen, moisture, light, contamination, and mechanical damage | Seal integrity, net weight, coding accuracy, and foreign-body detection | Retail packs, food-service formats, export cartons, and multipacks |
| Automation and Plant Utilities | Process integration and facility support | PLC or SCADA controls, clean-in-place systems, compressed air, chilled water, and heat-transfer systems | Maintains stable production, traceability, sanitation, and energy management | OEE, batch records, temperature logging, sanitation verification, and utility consumption | Small-batch, medium-scale, and high-throughput chocolate plants |